CPET Shrink Sleeves: Recycled in the RIC 1 PET Stream
How crystallizable PET sleeve film clears the float-sink tank and the dryer that trip other sleeve materials, and how to spec one that recovers with the bottle.
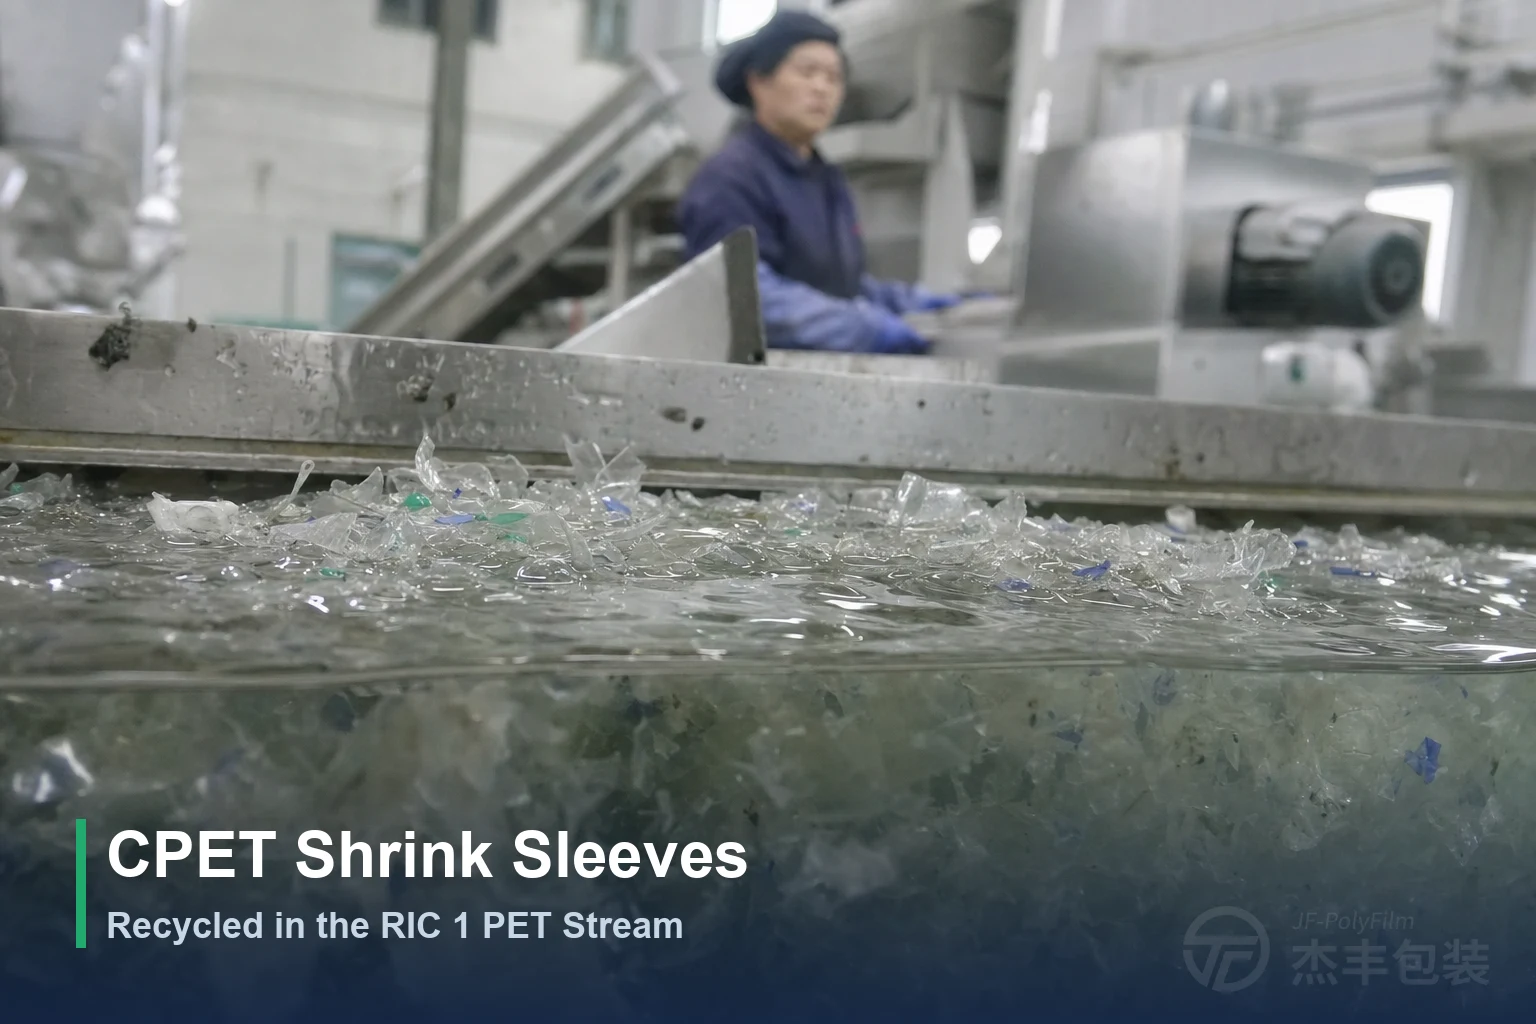
Whether a shrink sleeve is recyclable is settled by what the film is made of, not by the code on the bottle underneath. A CPET (crystallizable PET) sleeve is a crystallizable, PET-family film that runs amorphous on the labelling line — so it collapses cleanly onto the container — then crystallizes under the recycling dryer’s heat, so it holds its shape and recovers inside the RIC 1 PET stream with the container instead of downgrading it.
Key takeaways
- Inside a PET recycling plant a sleeve faces two separate physical tests: a float-sink tank that sorts by density, then a dryer that sorts by heat resistance. Clearing one says nothing about the other.
- Water in the tank sorts at 1.0 g/cm³: PET bottle flake at about 1.38 g/cm³ sinks and is collected, while polyolefin caps and floatable labels around 0.90–0.96 g/cm³ float off.
- Anything denser than water sinks into the PET fraction whatever polymer it is, so density alone decides the first gate — both PETG (1.28–1.33 g/cm³) and PVC settle in with it.
- The dryer is where chemistry, not weight, decides the outcome: PETG softens and clumps, while crystallizable PET crystallizes in the heat, holds its shape, and stays recoverable.
- A CPET sleeve clears both gates because it is PET-family (it sinks with the bottle) and crystallizable (it crystallizes in the dryer’s heat and survives it) — the one substrate that leaves a true mono-material PET package.
The two gates a sleeve has to clear inside a PET plant
Recyclability for a sleeve is not decided at a single step; it is decided at two, and passing the first says nothing about the second. After bottles are ground into flake and washed, the flake drops into a float-sink tank that sorts material by density, and the PET fraction it collects then moves through a heated dryer before it can be reused. Those two stages test a sleeve on different properties — weight at the tank, heat resistance at the dryer — so a film can sail through separation and still come apart under heat. The PET shrink sleeve recyclability overview maps the full set of sleeve designs and routes; the sections here stay on the two physical gates and on why crystallizable PET is the one material that clears both.
Gate one: the float-sink tank sorts by density
At the float-sink tank, separation comes down to one number — 1.0 g/cm³, the density of water. PET flake at roughly 1.38 g/cm³ settles to the bottom and is collected as the target fraction, while polypropylene and polyethylene caps and floatable labels at about 0.90–0.96 g/cm³ rise and are skimmed. Nothing here reads a resin code; the bath sorts purely by weight relative to water. That is what lets a low-density polyolefin label separate itself cleanly, and it is also what sends any sleeve heavier than water straight into the PET fraction, whether or not it belongs there.
| Material | Density (g/cm³) | In the water tank | Outcome in PET recycling |
|---|---|---|---|
| Water (the sorting line) | 1.00 | reference | sets the float/sink threshold |
| PP / PE caps & floatable labels | 0.90–0.96 | floats | skimmed off, recovered separately |
| PET bottle flake | ~1.38 | sinks | the target PET fraction |
| CPET sleeve | PET-family, ≈ bottle | sinks with the bottle | stays in PET, then clears the dryer |
| PETG sleeve | 1.28–1.33 | sinks with PET | enters PET, then fails at the dryer |
| PVC sleeve | close to PET | sinks with PET | contaminates the PET fraction |
Read down the sink rows and the problem announces itself: PETG and PVC settle in the same band as PET, so the water bath cannot tell the three apart and delivers all of them into one fraction. Density has done its job — it simply cannot distinguish a PET bottle from a sleeve that happens to weigh about the same. Everything those look-alike sleeves do next is decided at the second gate.
Gate two: the dryer sorts by softening point
The sorted PET fraction still holds wash water, so it passes through a heated dryer before it becomes usable flake, and heat sorts on a different axis than weight. What matters at this stage is the temperature at which a polymer begins to soften, and that is set by chemistry, not density. A flake that settled correctly with the PET still has to travel through the dryer without softening, sticking to its neighbors, or bleeding color into the flake around it.
A glycol-modified polymer such as PETG is engineered to resist crystallizing, the same trait that gives it a wide, forgiving shrink window on the labelling line. That resistance to crystallizing is also what pins its density near PET’s and carries it through the tank in the first place, so the failure never surfaces at gate one. It surfaces in the dryer, because a polymer that resists crystallizing also softens at a lower temperature. When PETG flakes reach the heated stage they can soften, fuse into clumps, and release their inks into the clear PET around them; the recovered flake then carries haze and color it should not have, and its grade drops.
Crystallizable PET does the opposite. Under the dryer’s heat it crystallizes, and that crystalline structure holds its shape to far higher temperatures, so the flakes stay loose and discrete through the dryer instead of clumping. This is the gate that density-only accounts of recyclability skip, and it is the one that separates a sleeve that genuinely recovers as PET from a glycol-modified film that only looked the part in the water tank.
Why PETG and PVC each break the PET stream
PVC and PETG both clear gate one by sinking with the PET, yet both still damage the recovered material — for different reasons, at different gates. Knowing which gate stops each one turns “avoid these” from a slogan into a mechanism you can reason from: PVC is caught at the density gate, PETG at the heat gate.
PVC fails quietly, at the density gate. It settles close enough to PET that the tank cannot separate the two, so it sinks into the PET fraction undetected and degrades the batch; even small amounts shift color and introduce defects during reprocessing. Recycling-design guides class PVC as rendering a PET package non-recyclable for exactly this reason.
PETG fails later, at the heat gate. It sinks correctly with the PET and passes separation cleanly, then causes its trouble in the dryer, where the lower softening point lets it clump and bleed ink into the recovered flake. The two are easy to confuse because both sink with PET, but PVC poisons the fraction it sinks into while PETG poisons the fraction it is heated in. A material-by-material comparison of the pair sits in the PETG vs PVC shrink film guide, and PETG’s strengths on the shelf — the clarity and shrink that make it the default decorative film — are covered on the clear PETG shrink film page.
Recovered with the bottle: why crystallizable PET clears both gates
Crystallizable PET is the one sleeve substrate that passes both gates by the single property that defines it. At gate one it sinks with the bottle because it is a PET-family resin, dropping straight into the target fraction. At gate two it stays intact because, once it crystallizes under the dryer’s heat, that crystallinity raises the temperature at which the polymer softens, so the flakes hold their shape through the dryer rather than fusing. One material, two gates, and no separation step in between.
That is what makes it a genuine mono-material outcome rather than a marketing one. A low-density polyolefin sleeve can also call itself “recyclable,” but it gets there by the opposite physics — it floats clear of the sinking PET and is recovered in a separate polypropylene or polyethylene stream. That float-and-remove route is well established and clean at separation, yet its end state is two polymers sorted apart, not one recovered together. For a program built around mono-material PET packaging, recovering a single polymer with the bottle is the structurally simpler result, and that is the case crystallizable PET makes. JFPolyFilm’s CPET shrink film carries a 230°C melting point, well above the temperatures a standard bottle-recycling dryer reaches, which is the margin that keeps the film solid where a lower-softening sleeve would fuse.
Decoration follows the same logic. Print run with wash-off inks lifts off during the hot caustic wash instead of coloring the recovered flake, so a crystallizable PET sleeve recovers clean both as a substrate and as a printed surface — completing the RIC 1 PET stream with the bottle it was applied to.
Recyclable is not the same as recycled content
One distinction is worth drawing before any of this reaches a sustainability brief, because buyers merge the two constantly. Recyclability is an end-of-life property — whether the film can re-enter a recovery stream after use, the entire subject above. Recycled content is an input property — how much already-reclaimed material went into making the film in the first place. A sleeve can satisfy one, both, or neither. Crystallizable PET answers the end-of-life question by being recoverable in the RIC 1 PET stream, and says nothing about what it was originally made from; recycled content runs on a separate track, measured as a percentage of reclaimed material and verified through a supply-chain scheme such as the Global Recycled Standard. A film built with verified reclaimed PET — the ground the RPET shrink film covers — carries that credential independently of whether it is itself recyclable at end of life. State the two claims separately, because asking for one does not deliver the other.
Speccing a sleeve that recovers with the bottle
Specifying a sleeve that genuinely recovers with the bottle comes down to a handful of material and print choices, each tied to a gate the film has to clear. Every line below is something a supplier can confirm rather than a promise to take on trust.
- A mono-material PET substrate. A PET sleeve is recovered with the bottle; a look-alike polymer has to be sorted out or floated off. The first question is whether the film genuinely recovers in the PET stream — a crystallizable, PET-family substrate — rather than a look-alike grade that only resembles it.
- Heat resistance verified through the dryer. The substrate has to hold together at drying temperatures without clumping — the property that separates crystallizable PET from glycol-modified PETG. A published melting point above bottle-recycling dryer temperatures, the 230°C figure noted above being the kind of marker to ask for, confirms the film clears the heat gate.
- Wash-off decoration. For a film that sinks with the PET, the print should release in the caustic wash instead of tinting the recovered flake. Direct-print processes such as gravure, flexographic, and UV-inkjet are compatible, and high-surface-energy CPET grades, ours included, print directly without corona pre-treatment.
- Shrink matched to the bottle. The sleeve has to grip the container’s contours to apply cleanly and stay square. A high transverse shrink with little machine-direction movement — TD of 74±2% with MD held to ≤5% on the JFPolyFilm CPET grade — keeps the graphics undistorted as the film conforms.
- Acceptance confirmed per market. Collection and sortation differ by region and are never universal, so the construction should be checked against the systems in each destination before a recyclability claim is made. Recyclers increasingly judge a design against a published guide such as the APR Design Guide in North America or RecyClass in Europe, and that evaluation is worth requesting from the supplier.
Recovering the sleeve with the bottle is a property of these choices, not a label claim, and each point above is a checkable line item. For sleeves built to complete the RIC 1 PET stream, the JFPolyFilm CPET shrink film is engineered for the sink-and-recover route at 30–60 μm in widths to 2000 mm; send the bottle, line speed, and target markets, and our team can confirm the fit against a given recyclability requirement.
Frequently Asked Questions
Is a CPET shrink sleeve recyclable together with the bottle?
Why does CPET survive PET recycling when PETG does not?
Does a CPET sleeve have to be removed before the bottle is recycled?
Why does PVC shrink film ruin PET recycling?
Is a recyclable sleeve the same as a sleeve with recycled content?
Related Articles
How to Store Shrink Film: Rolls, Shelf Life, Handling
What the 10–30°C, 12-month storage window actually protects, how to stand rolls so they don't flat-spot, and why film has to acclimate before it reaches the line.
Shrink Film Test Methods: How Specs Are Measured
Every figure on a shrink film datasheet or COA traces back to a standard method. See which ASTM and ISO tests measure shrinkage, tensile, haze, and gauge, and how to read the report.
Need Expert Advice on Shrink Film?
Our technical team can help you choose the right film for your application.
Contact Us